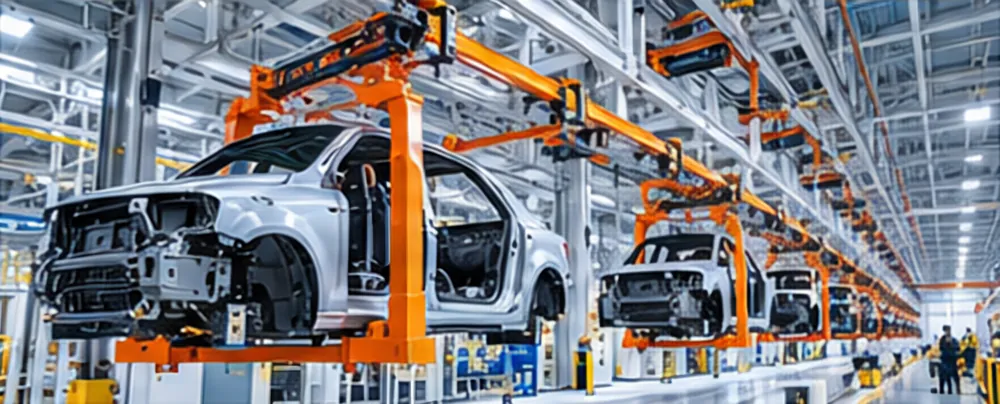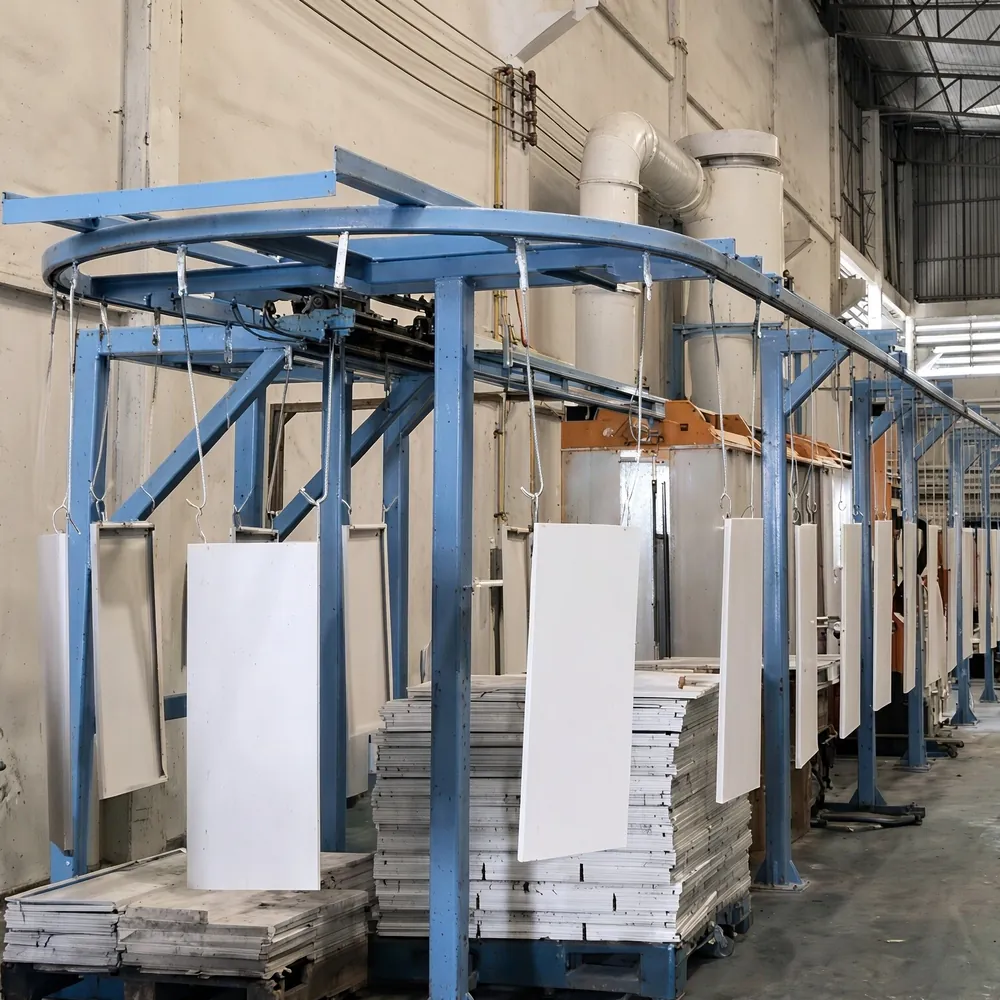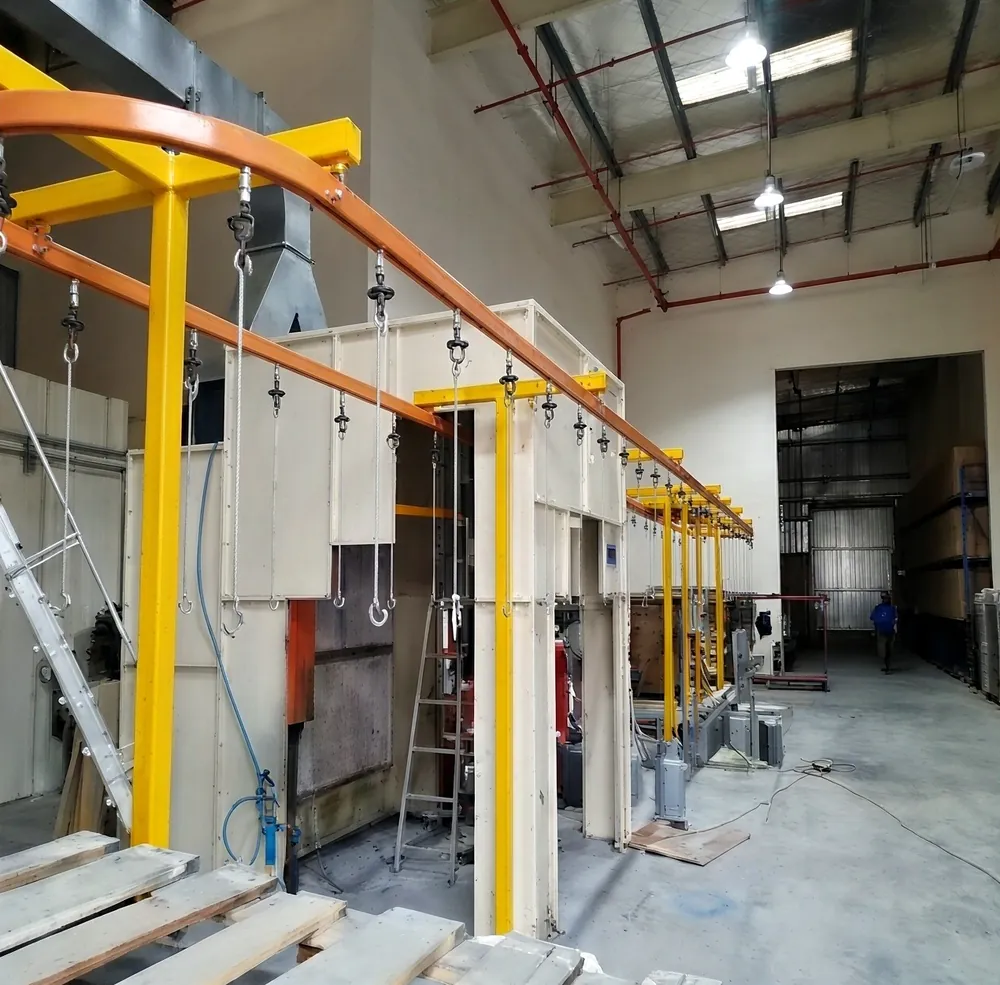
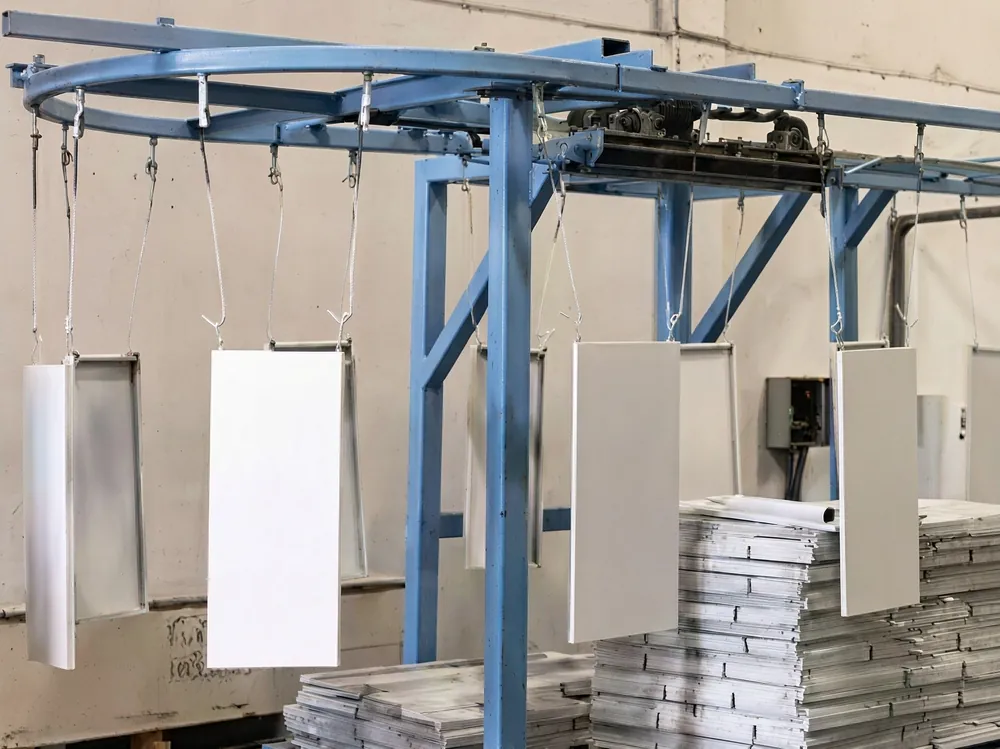
Floor conveyors include belt, roller, chain, pallet and skid systems. Overhead conveyors carry products on hangers from a track above. Both are proven; each fits different needs.
Side-by-side
| Criteria | Overhead conveyor | Floor conveyor |
|---|---|---|
| Floor space | Floor stays free | Occupies floor area |
| Access to product | Hanging parts open on most sides | Top and sides open; bottom on the conveyor |
| Product types | Parts that can hang | Boxes, pallets, flat or unstable products |
| Coating and drying | Ideal: all-round access | Limited |
| Crossing aisles | Passes over aisles | Needs gates, bridges or tunnels |
| Building | Needs roof or support steel capacity | Needs floor capacity |
| Height changes | Easy with inclines and lifts | Needs lifts or spirals |
Choose overhead when
- Parts must be coated, washed or dried on all sides
- Floor space is limited or needed for other work
- The route must cross aisles or other equipment
- Parts are long, large or irregular and hang naturally
Choose floor conveyors when
- Products are boxes, totes or pallets
- Products are unstable or cannot hang
- Heavy products must be positioned very precisely at floor level
- The building cannot carry overhead loads
Combining both
Many plants link the two: products travel overhead through coating and buffers, then transfer to floor conveyors for assembly or packing. Lift and drop stations make the transfer; see lift and lower stations and skid vs overhead conveyors.
Questions to ask your supplier
- Which product types will travel on the line, now and later?
- What are the floor and roof load limits?
- Where must the line cross aisles or other equipment?
- Where do products transfer between systems?
Common mistakes to avoid
- Choosing overhead without checking roof capacity
- Choosing floor conveyors for parts that must be coated on all sides
- Ignoring how the line crosses aisles and fire routes
- No plan for transfers between overhead and floor systems
Worked example: a mixed solution
An appliance plant paints steel housings and then assembles them. The coating line uses an overhead power and free conveyor so housings hang open for pretreatment, powder and curing. After unloading, a lift station lowers each housing onto a pallet conveyor for assembly, where operators need a stable, flat base at bench height.