Solutions
Line Balancing
We match conveyor speed, carrier pitch and station layout to your takt time, so every station gets the right amount of time and no carrier waits without reason.
From Takt Time to Conveyor Speed
Line balancing starts with takt time: the time available per unit to meet demand. The conveyor then has to deliver one carrier per takt to each station.
Conveyor speed = carrier pitch ÷ takt time
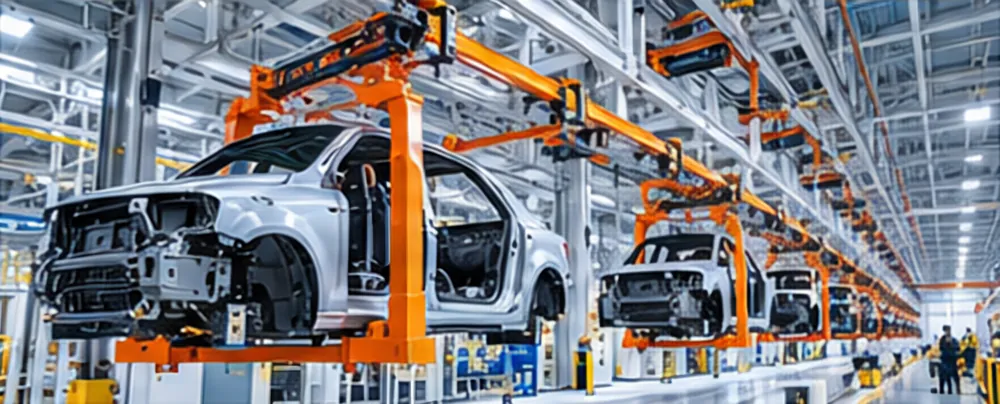
Example: at 30 jobs per hour the takt is 120 seconds. With a 6 m carrier pitch, a continuous line must move at 3 m per minute. For stop-and-go lines, EMS carriers move fast between stations and stop for the work content.
We also plan for model mix, where different products need different work times at the same station.
How We Do It
Tools for a Balanced Line
Throughput calculation
Jobs per hour, pitch, speed and station count calculated before design.
Continuous or indexing
Moving-line assembly or stop-and-go stations, chosen per process.
Variable speed zones
EMS carriers slow down in work zones and speed up in transport sections.
Model mix support
Parallel stations and bypasses for products with longer work content.
Buffer placement
Small buffers between zones to absorb variation in work time.
Simulation
Flow checks of the layout before steel is cut, to confirm the target output.
FAQ
Frequently Asked Questions
What is takt time?
Takt time is the available production time divided by customer demand. For example, 3,600 seconds per hour divided by 30 units gives a takt of 120 seconds.
How do you calculate conveyor speed?
For a continuous line, divide the carrier pitch by the takt time. A 6 m pitch at a 120-second takt gives 3 m per minute.
How do you handle different products on one line?
With model mix planning: parallel stations, bypasses and variable speed zones give longer work content more time without slowing the whole line.
Explore
Related Solutions
Planning a New Production Line?
Let our engineers design the right conveyor solution for your application.
WhatsApp Us Discuss Your Project