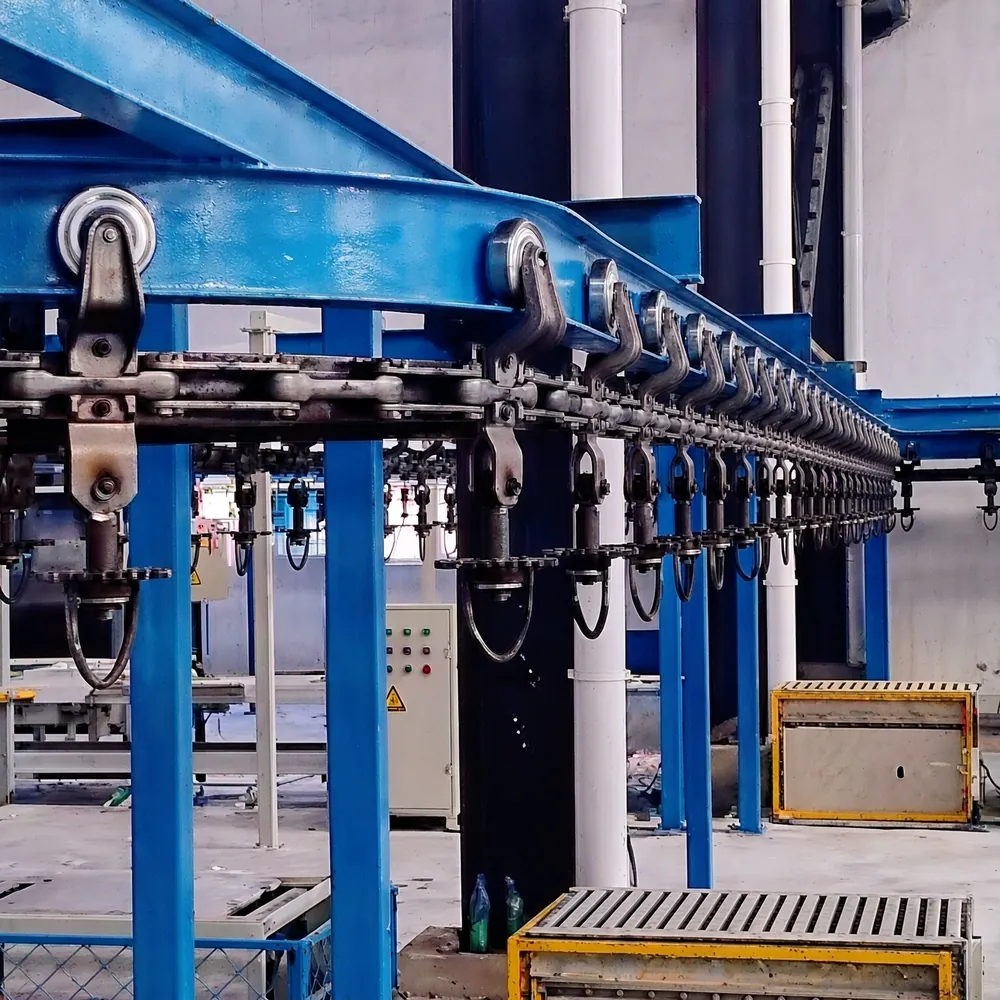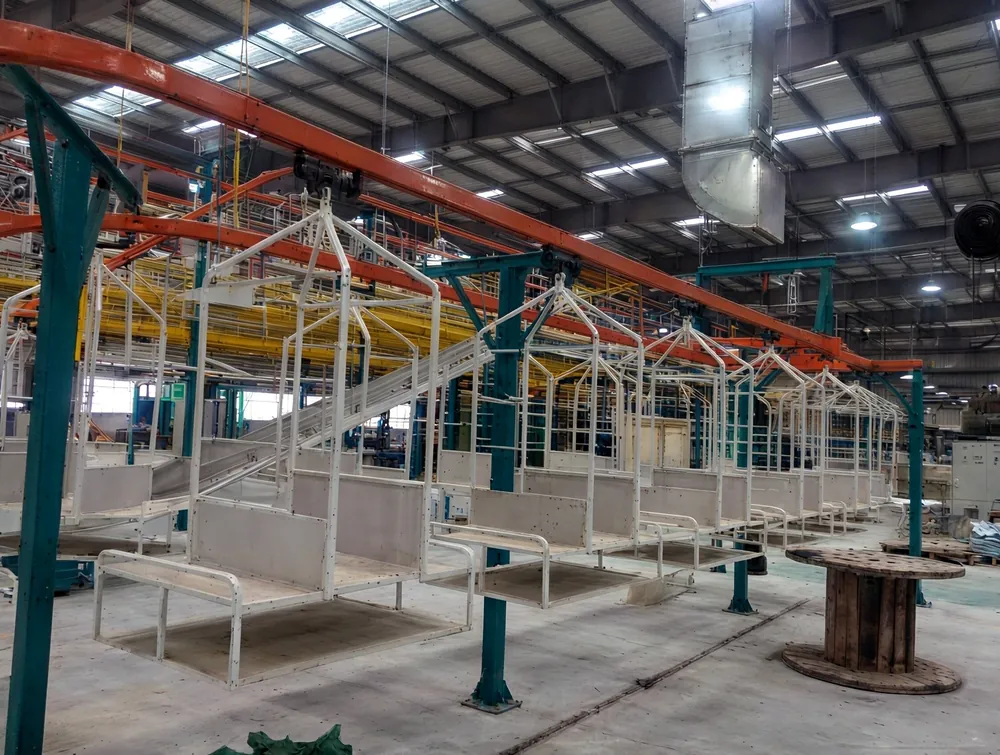
A powder coating line is a chain of processes: loading, pretreatment, dry-off, powder booth, curing oven, cooling and unloading. The overhead conveyor links them, so the layout is really the design of the conveyor route.
The zones in order
| Zone | Layout consideration |
|---|---|
| Loading | Close to the unloading area and to incoming parts |
| Pretreatment | Spray tunnel or dip tanks; drainage and chemical supply |
| Dry-off oven | Directly after pretreatment |
| Cooling before booth | Parts must cool before powder application |
| Powder booth | Clean air, colour change space, gun access |
| Curing oven | Length set by line speed and dwell time; often several passes |
| Cooling | Enough length or forced air before unloading |
| Unloading and inspection | Next to loading to share labour |
Common layout shapes
| Layout | Strengths | Watch out for |
|---|---|---|
| U-shape or loop | Loading and unloading together; compact | Return run must fit beside the process |
| Straight-through | Simple flow, easy to extend | Long building; loading and unloading far apart |
| Multi-pass ovens | Long dwell in a short oven | More curves and track inside the oven |
| Power and free with buffers | Batching and colour changes | More floor or overhead space for lanes |
Sizing the layout
Line speed and dwell times set the conveyor length in each zone:
Zone conveyor length = line speed × time in zone
Example: at 1.5 m/min, a 20-minute cure needs 30 m of conveyor in the oven; with a 10 m oven, the conveyor makes three passes. Pretreatment stages, dry-off and cooling are sized the same way. See powder coating conveyor systems for line speed and hanging density.
The support structure
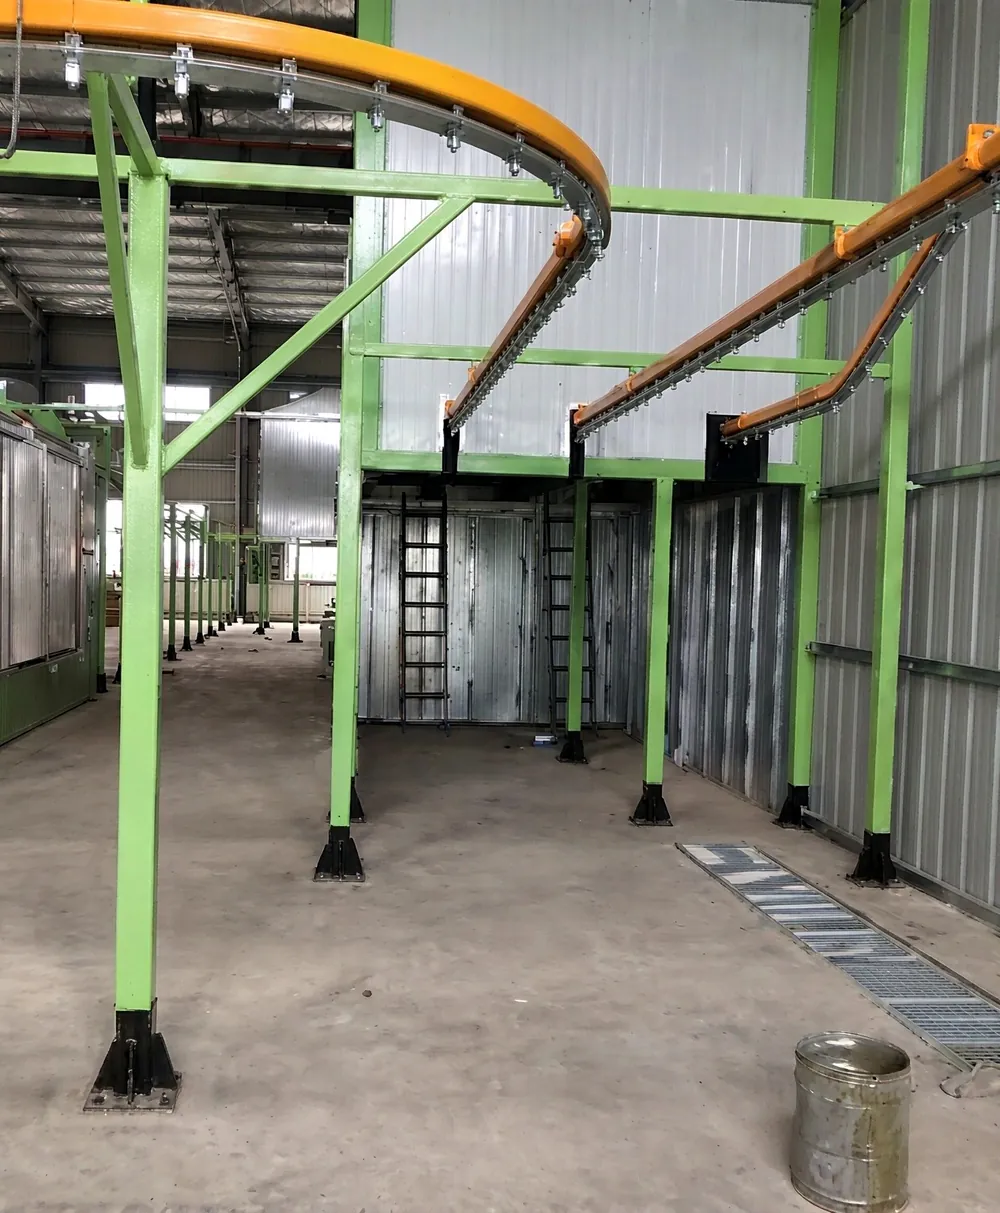
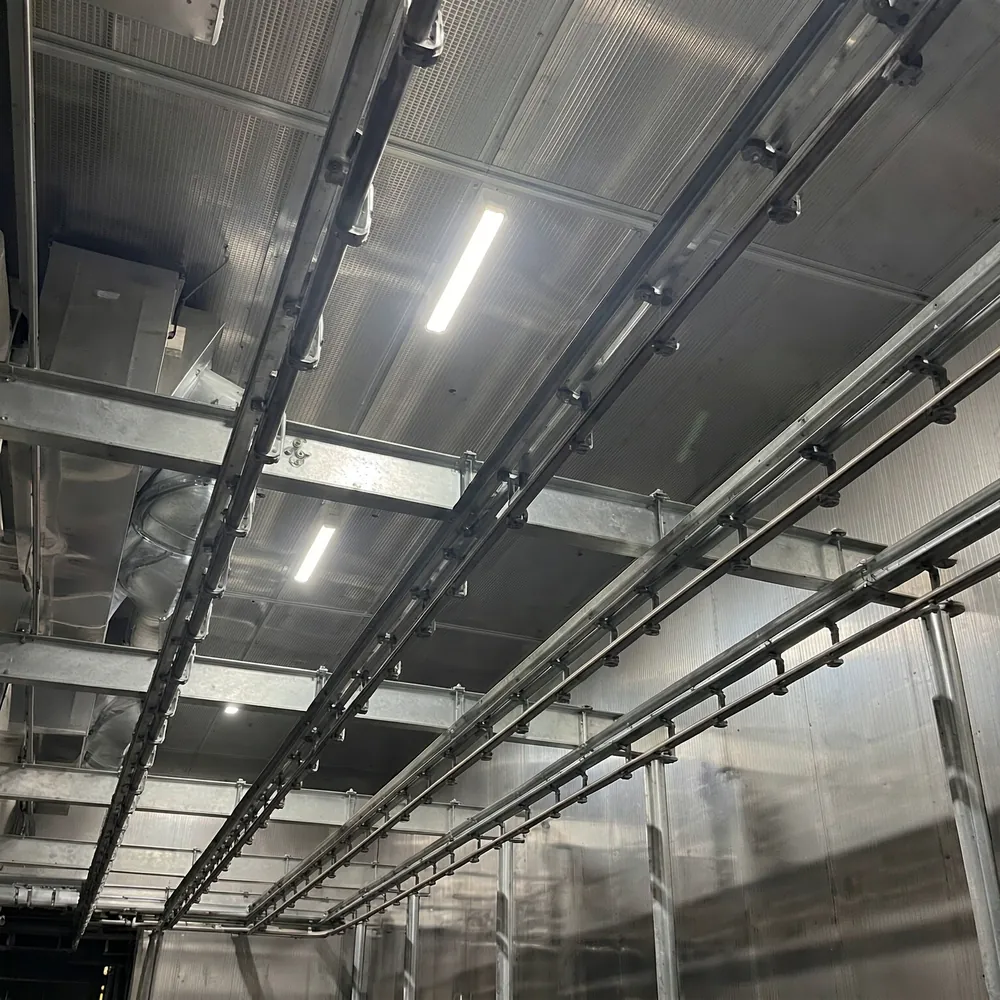
Many powder coating lines run on a freestanding steel structure rather than hanging from the roof. It carries the track over the processes and into the enclosures, and it can be built before the roof is checked or reinforced. Read overhead conveyor support steel.
Layout mistakes to avoid
- Loading and unloading far apart, doubling labour
- No cooling before the booth, so powder cures early on hot parts
- Curves and drives inside the oven where they are hard to service
- No space for a second booth or colour change
- No room to extend the line when volumes grow
HITREE designs conveyors for surface treatment lines. Send us your building drawing and output for a layout proposal.
Worked example: a U-shaped powder coating line layout
A plant has a hall 60 m long and 24 m wide. A straight line would put loading at one end and unloading at the other, 60 m apart. A U-shaped powder coating line layout runs pretreatment and dry-off along one side, the booth and oven at the far end, and cooling back along the other side, so loading and unloading sit next to each other near the dispatch door. One team handles both, and empty hangers return over a short distance.
Powder coating line layout checklist
| Topic | Check |
|---|---|
| Flow | Loading and unloading close together; no crossing material flows |
| Zones | Conveyor length per zone calculated from speed and time |
| Utilities | Gas, power, water and exhaust routes to ovens and pretreatment |
| Access | Maintenance access to drives, take-ups and booth |
| Expansion | Space for a second booth or longer oven |