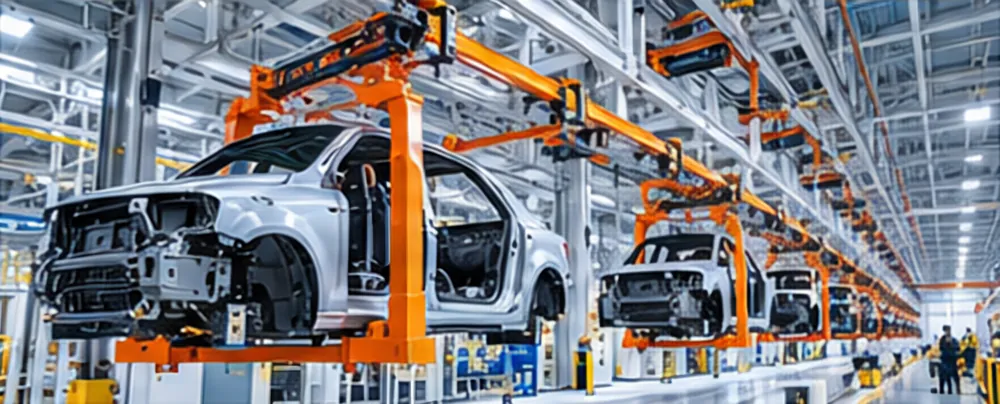
An overhead conveyor layout ties together your products, processes and building. Getting the basic numbers right early prevents expensive changes later.
1. Collect the input data
- Product dimensions, weight and handling points
- Target output in jobs per hour and working shifts
- Process stations and their cycle times
- Building drawings with column grid, roof structure and clear heights
- Existing equipment, aisles and fire safety zones
2. Calculate the takt time
Takt time is the time available per unit. It sets the rhythm of the whole line.
Takt time = available time ÷ required units
Example: 3,600 seconds per hour ÷ 30 jobs per hour = 120 seconds per job.
3. Choose carrier pitch and conveyor speed
Carrier pitch is the distance between carriers. It depends on product length plus a safe gap, and on curves and switches in the route.
Conveyor speed = carrier pitch ÷ takt time
Example: with a 6 m pitch and a 120-second takt, a continuous line runs at 6 m ÷ 2 min = 3 m per minute.
4. Size the buffers
Buffers absorb stoppages between processes. A simple first estimate:
Buffer carriers ≈ stoppage to bridge ÷ takt time
To bridge a 10-minute stoppage at a 60-second takt, plan around 10 carriers plus margin. See accumulation and buffering.
5. Count the carriers
Total carriers = carriers in process zones + buffer carriers + carriers on return and transport sections. Carrier count drives cost, so we optimise route length and buffer size together.
6. Check the building
- Roof or ceiling can carry the conveyor loads, or a support structure is planned
- Clear heights allow the load to pass over aisles and equipment
- Crossing points with cranes, doors and fire shutters are resolved
- Access for installation and later maintenance is available
7. Confirm with simulation
For complex lines with buffers, model mix and several routes, a flow simulation confirms the layout reaches the target output before fabrication starts.
Need help with your layout? Send us your drawings and our engineers will review them.