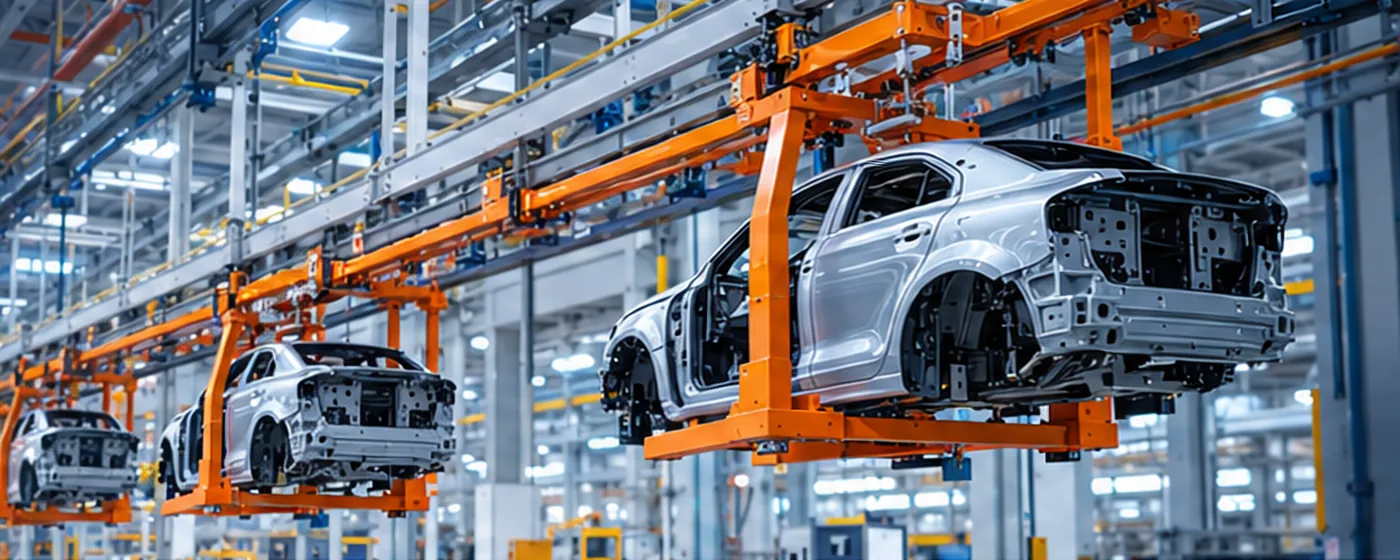
Buying an overhead conveyor from China can lower the equipment budget and shorten fabrication time. The projects that go well have one thing in common: the buyer treats sourcing as an engineering project, not a purchase order.
This guide covers the full process, from shortlisting manufacturers to start-up, for power and free conveyors, EMS overhead conveyors and other overhead systems.
Why plants source overhead conveyors from China
- Competitive equipment cost for steel structures, track, carriers and fabrication
- Large fabrication capacity and short manufacturing lead times
- Experience from high-volume automotive, appliance and coating plants in China
- Suppliers able to deliver complete lines: mechanics, electrics and controls
The trade-offs are distance, time zones, shipping and the need for on-site support far from the factory. A good supplier plans for all four from the start.
Step 1: Define what you are buying
Before contacting suppliers, write a short requirement specification. It makes quotes comparable and prevents scope gaps later.
- Products: dimensions, weight, hanging or support points
- Output: jobs per hour, shifts, planned growth
- Process: stations, ovens, wet areas, buffers, load and unload heights
- Building: layout drawing, column grid, clear heights, roof load limits
- Standards: CE for Europe, ASME B20.1 for the US, local electrical codes
- Preferred PLC brand and component brands stocked in your country
- Delivery term (for example FOB or DAP) and installation scope
Our layout planning guide explains the throughput numbers to include.
Step 2: Shortlist manufacturers, not traders
Many listings on B2B marketplaces are trading companies. For an engineered conveyor you need direct access to the design team. Ask each candidate:
- Which parts do you design and fabricate in-house?
- Can our engineers talk directly to your project engineer in English?
- Can you share layouts and videos of comparable lines?
- Who installs and commissions abroad, and how is that organised?
Use our 10-question supplier checklist to compare answers.
Step 3: Audit the factory
Visit the factory or ask for a live video audit. Look for:
| Area | What to check |
|---|---|
| Engineering | 3D design tools, load calculations, drawing control, an engineer assigned to your project |
| Fabrication | Cutting, welding and machining capacity; jigs for track and carriers |
| Quality | Incoming inspection, dimensional checks, weld inspection, records |
| Assembly and test | Space to pre-assemble drives, switches and lifts; test benches for panels |
| Controls | In-house panel building and PLC programming, or a named partner |
| Logistics | Export packing, part marking, packing lists |
Step 4: Agree the technical proposal
The proposal should include a layout drawing, throughput calculation, chain class and track type, carrier design, control concept, and a clear list of what is included and excluded. Do not compare totals until scopes match. Our price and cost guide lists the items a complete quotation should contain.
Step 5: Contract, payment milestones and acceptance
Engineered conveyors are usually paid in milestones tied to progress, for example a deposit on order, a payment after a successful factory acceptance test or before shipment, and a final payment after site acceptance. Define both acceptance tests in the contract, including the output the line must reach.
Step 6: Quality control and factory acceptance test
Ask for pre-assembly and function tests of drives, switches, stops, lifts and control panels before shipment. Attend the factory acceptance test in person or by video, and approve the punch list before packing.
Step 7: Shipping and import
- Agree the Incoterm and who arranges freight and insurance
- Confirm packing for sea freight: rust protection, crates, part marking by area
- Check the HS code and import duty with your customs broker (conveyors generally fall under HS heading 8428)
- Plan unloading, storage on site and the order in which crates are needed
Step 8: Installation and commissioning
Choose between installation by the manufacturer's team, local installers under its supervision, or a fully local team. Supervision by the manufacturer's engineers is often a good balance of cost and risk. Plan visas, travel, lifting equipment and access platforms early. See our overhead conveyor installation guide.
Step 9: After-sales support
Before signing, agree the spare parts list, lead times, documentation in English, remote support for the controls and response times. Specifying motors, bearings and PLCs that are available in your country makes local support much easier.
Working with HITREE
HITREE designs and manufactures overhead conveyor systems and supports projects worldwide. Send your layout and output target to sale@hitreeconveyor.com, via WhatsApp or through our project inquiry form, and our engineers will reply within one working day.
Common mistakes when buying overhead conveyors from China
- Choosing on total price before the scopes are equal
- Leaving installation, controls or carriers "to be discussed later"
- Accepting component brands that are not stocked in your country
- No written factory acceptance test procedure
- No clear owner for the interface between the conveyor and your other equipment
Questions to ask an overhead conveyor manufacturer in China
| Question | Good answer includes |
|---|---|
| How did you size this line? | Takt time, pitch, chain speed and buffer calculation shown |
| Which chain class and track type? | A named class (for example 4 in) and the reason for it |
| Who is our project engineer? | A named engineer who joins technical calls |
| How is equipment tested before shipping? | Pre-assembly, function tests and a FAT report |
| What is excluded? | A written list: civil work, utilities, permits, local labour |
| How do you support us after start-up? | Spare parts list, remote access, response times |
A good overhead conveyor manufacturer answers these in writing. Vague answers in the quotation phase usually become problems on site.