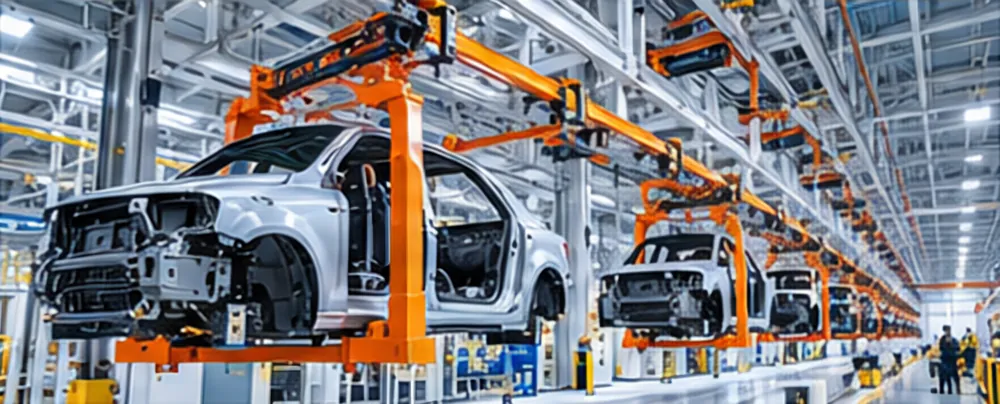
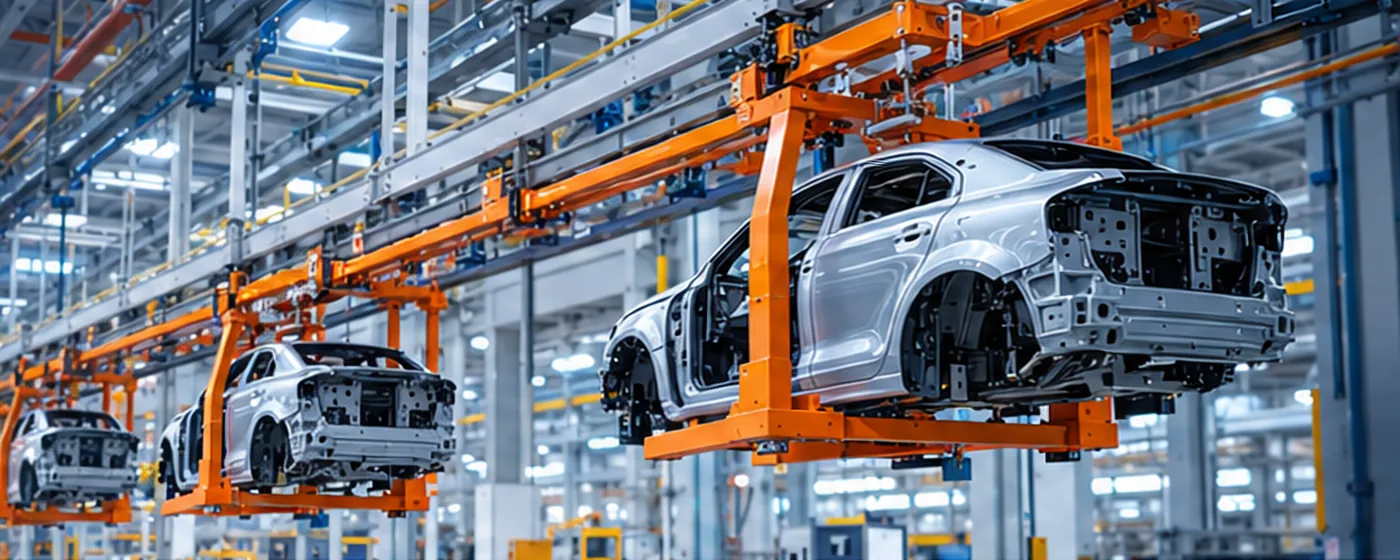
In an automotive or industrial paint shop, the conveyor carries every product through pretreatment, coating, curing and inspection. It must run reliably in water, chemicals, overspray and heat, without contaminating the finish.
Paint shop zones and conveyor needs
| Zone | Conveyor requirement | Common choices |
|---|---|---|
| Pretreatment | Corrosion resistance, drip control, dip or spray motion | Overhead or power and free with dip sections, dip systems |
| E-coat | Controlled immersion and exit, electrical contact | Power and free with drop sections, dip systems |
| Sealing and underbody | Stops, good access, ergonomic height | Power and free, skids, EMS |
| Paint booths | Steady speed, clean conveyor, robot access | Inverted power and free, skid conveyors |
| Ovens | Heat-rated parts, controlled dwell time | Power and free, oven chain conveyors, skids |
| Inspection and repair | Stops, bypass and repair loops | Power and free, skids |
| Painted body storage | Buffering and resequencing | Power and free lanes, skid lanes |
Overhead and inverted power and free in paint shops
Power and free conveyors handle the whole range of paint shop duties: accumulation between processes, routing to repair loops and passage through ovens. Inverted power and free is often preferred in booths because the chain and lubricant are below the product. Read more about inverted power and free.
Skid conveyors
Many automotive paint shops carry bodies on skids over roller beds, lifts and turntables. Skids give a stable, clean platform and precise positioning. Read the comparison in skid conveyor vs overhead conveyor.
Five design rules for paint shop conveyors
- Protect the finish: keep chain and lubricant away from wet and fresh paint; use covers and drip pans
- Control the dwell: calculate conveyor length in each process and oven from line speed and process time
- Buffer between processes: booths, ovens and repair run at different rhythms; buffers keep them independent
- Plan for repair: provide a route that takes defective products out and back into sequence
- Keep it serviceable: place drives and take-ups where they can be reached without entering hot or clean zones
Throughput and buffers
Paint shops lose output when one zone stops the others. Size buffers from the stoppages you want to bridge and the takt time; our accumulation and buffering page shows the method, and painted body storage explains the buffer between paint and assembly.
Related guides
For specific zones, see the e-coat conveyor guide, the curing oven conveyor guide and the powder coating conveyor guide. HITREE designs conveyors for surface treatment; contact us with your paint shop layout.
Worked example: buffers in a paint shop
A paint shop runs at 45 jobs per hour, a takt of 80 seconds. Booth cleaning and colour changes cause stops of up to 8 minutes. To keep the oven and inspection running through such a stop, the buffer before the booth must hold 8 × 60 ÷ 80 = 6 carriers, plus a margin. After the oven, a second buffer protects the booth from short stops at inspection.
Questions to ask a paint shop conveyor supplier
- Which conveyor type do you propose for each zone, and why?
- How do you keep chain lubricant away from wet and fresh paint?
- How is dwell time in each process and oven controlled?
- Where are the buffers and how were they sized?
- How do repair loops return products into the sequence?
- How are drives and take-ups reached for maintenance?
Paint shop conveyor terms
| Term | Meaning |
|---|---|
| Dwell time | Time a product spends in a process zone or oven |
| Drop section | Track section that lowers carriers into a process or to a station |
| Repair loop | Route that takes defective products out and back into flow |
| Flash-off | Zone where solvents evaporate before the oven |
A good paint shop conveyor system balances finish quality, throughput and maintenance access.